Consulting Projects & Industrial Case Studies
Explore verified case studies showcasing proven energy savings, boiler stack condensing heat recovery, steam trap modernizations, and rigorous Aspen HYSYS / Plus simulation models.
From green steel transition kinetics to refinery Pinch HEN networks and brewery heat recovery.
Featured Case Studies & High-Impact Outcomes
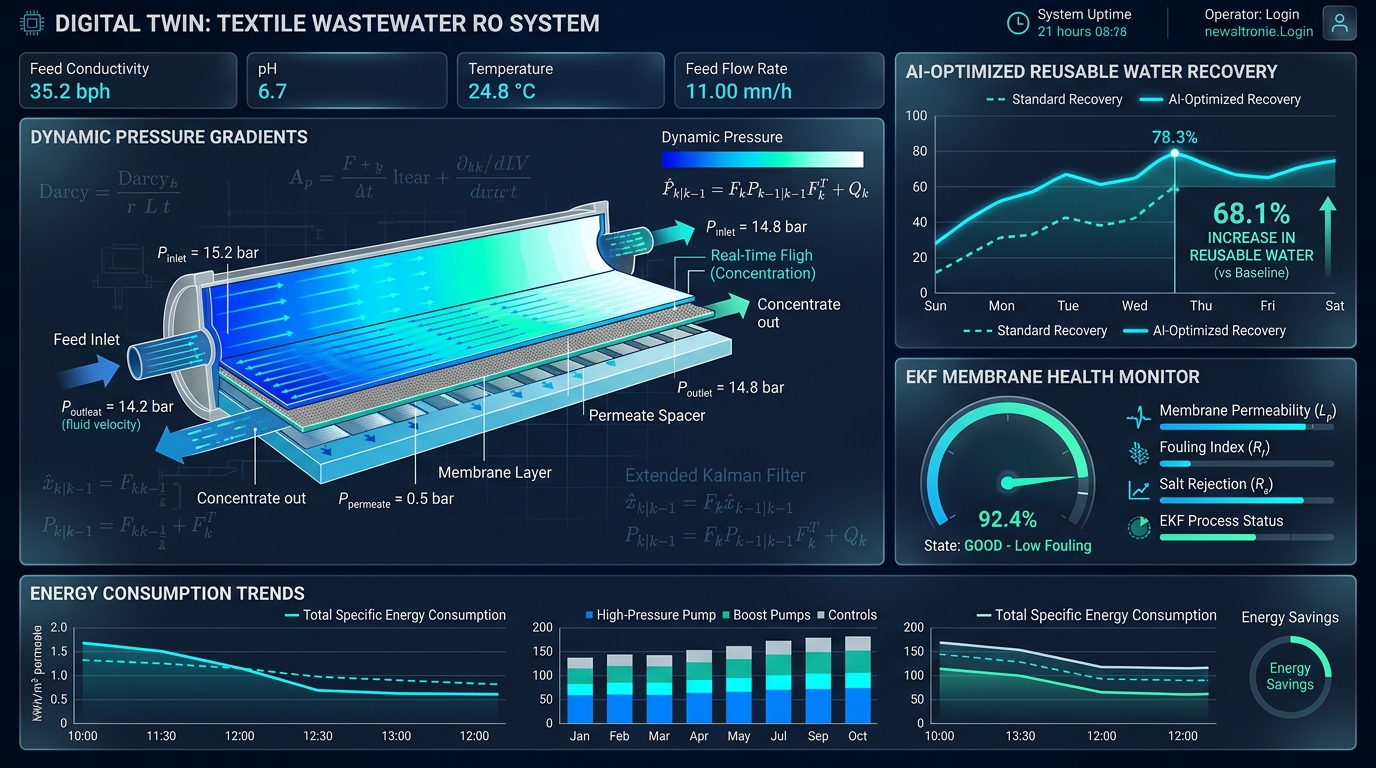
WaterTwin AI: Predicting Membrane Fouling to Optimize Industrial Wastewater Reuse
Optimizing Lactic Acid Fermentation: From Experimental Bioreactor Data to an Operating Strategy
Where Is the Energy Going? Optimizing Lead-Acid Battery Formation with Data Analytics
Filter Case Studies
(Showing 22 of 22)Process systems engineering and industrial AI digital twin for textile wastewater reverse osmosis (RO), combining a first-principles solution-diffusion model, dynamic fouling kinetics, Extended Kalman Filter (EKF) state estimation, and 24-hour predictive cleaning optimization.
A process-engineering study using experimental bioreactor data for Lactobacillus delbrueckii subsp. bulgaricus CFL1 to evaluate how temperature, pH, and harvest stage govern lactic acid titer, batch kinetics, and apparent volumetric productivity.
A data-driven chemical/process engineering investigation analyzing electricity consumption across 12,286 lead-acid battery formation batches using specific energy metrics, connector resistance, and interruption data to identify energy inefficiencies and theoretical reduction opportunities.
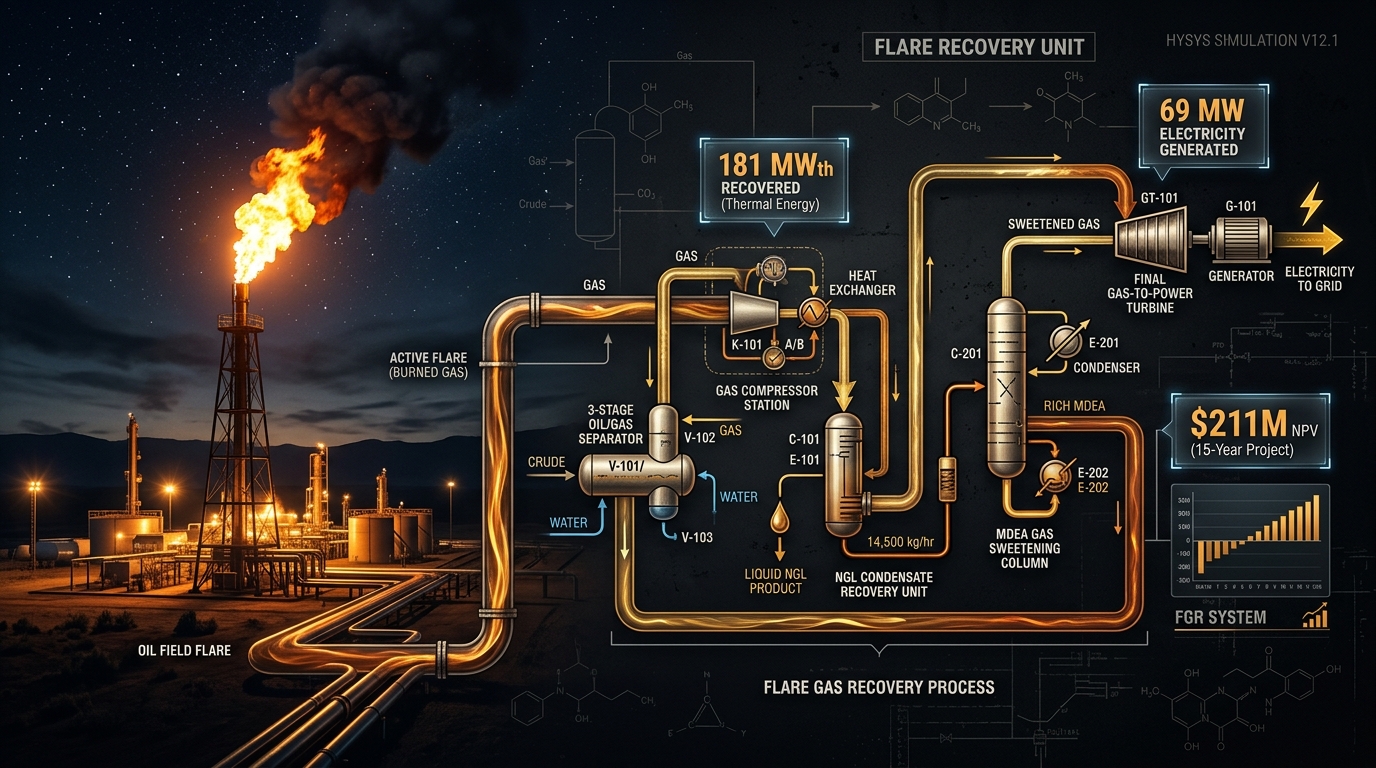
Aspen HYSYS process simulation and screening techno-economic analysis investigating the transformation of routine associated gas flaring into commercial energy assets: 3-stage separation, multi-stage compression, NGL recovery, MDEA amine sweetening, and Gas-to-Power vs Pipeline Sales.
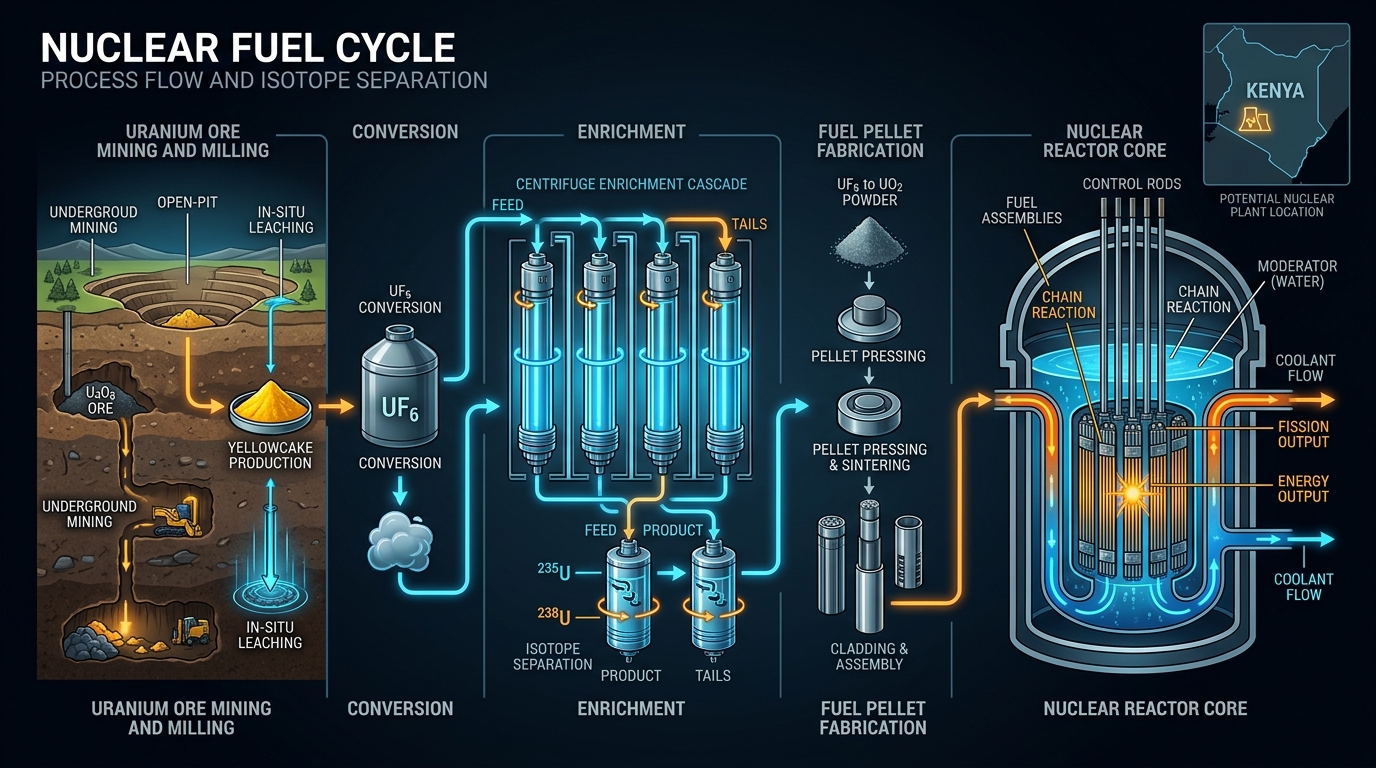
Aspen Plus chemical engineering case study and infrastructure readiness evaluation exploring the nuclear fuel cycle—from natural uranium mining, conversion to UF₆, and gas centrifuge isotope enrichment (U-235/U-238) to ceramic UO₂ fuel pellet fabrication and Kenya's regulatory, grid, and nuclear safety readiness.
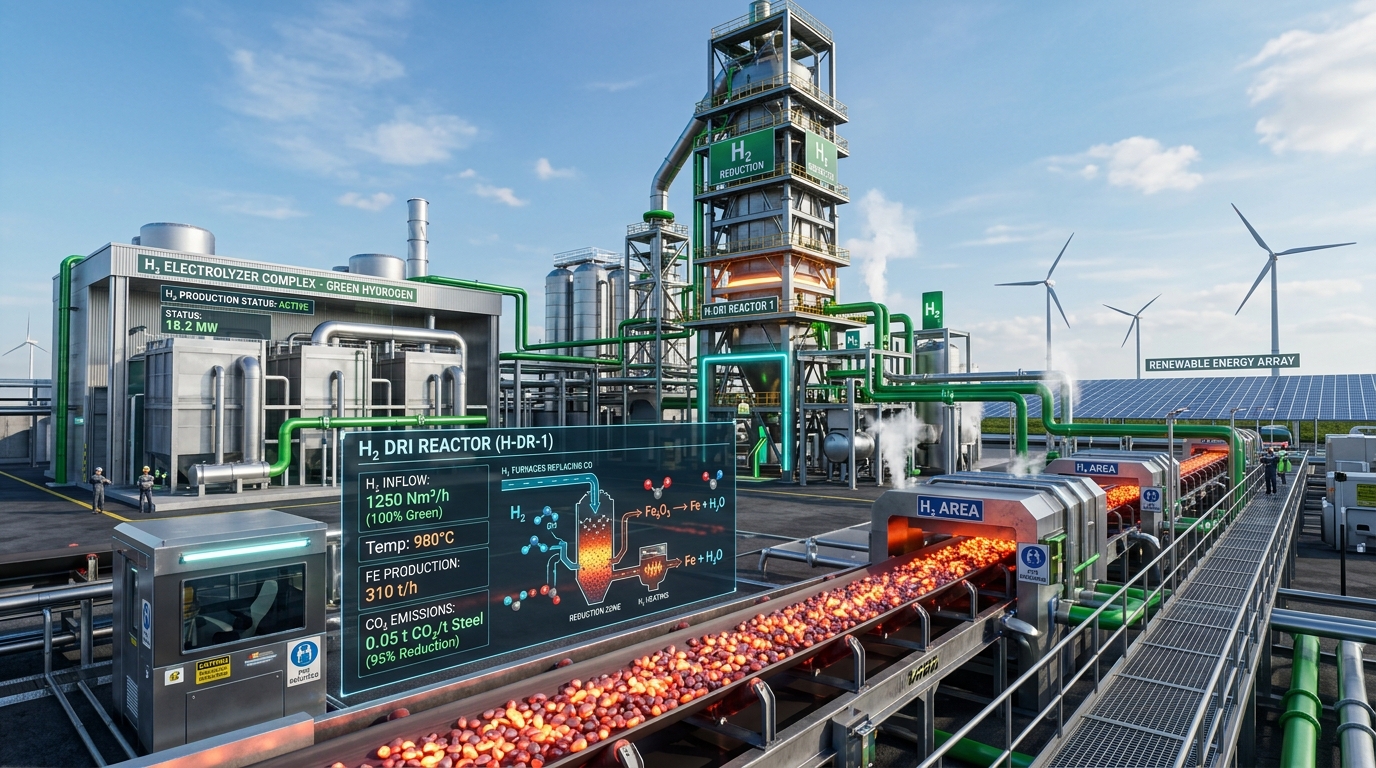
Aspen Plus process simulation and digital decision-support platform evaluating 5 progressive hydrogen transition pathways (NG100 → H25 → H50 → H75 → H100) for a 119 t/h metallic iron plant, optimizing trade-offs between process CO2 abatement, electrolyzer MW scale-up, renewable power tariffs, and capital investment constraints.
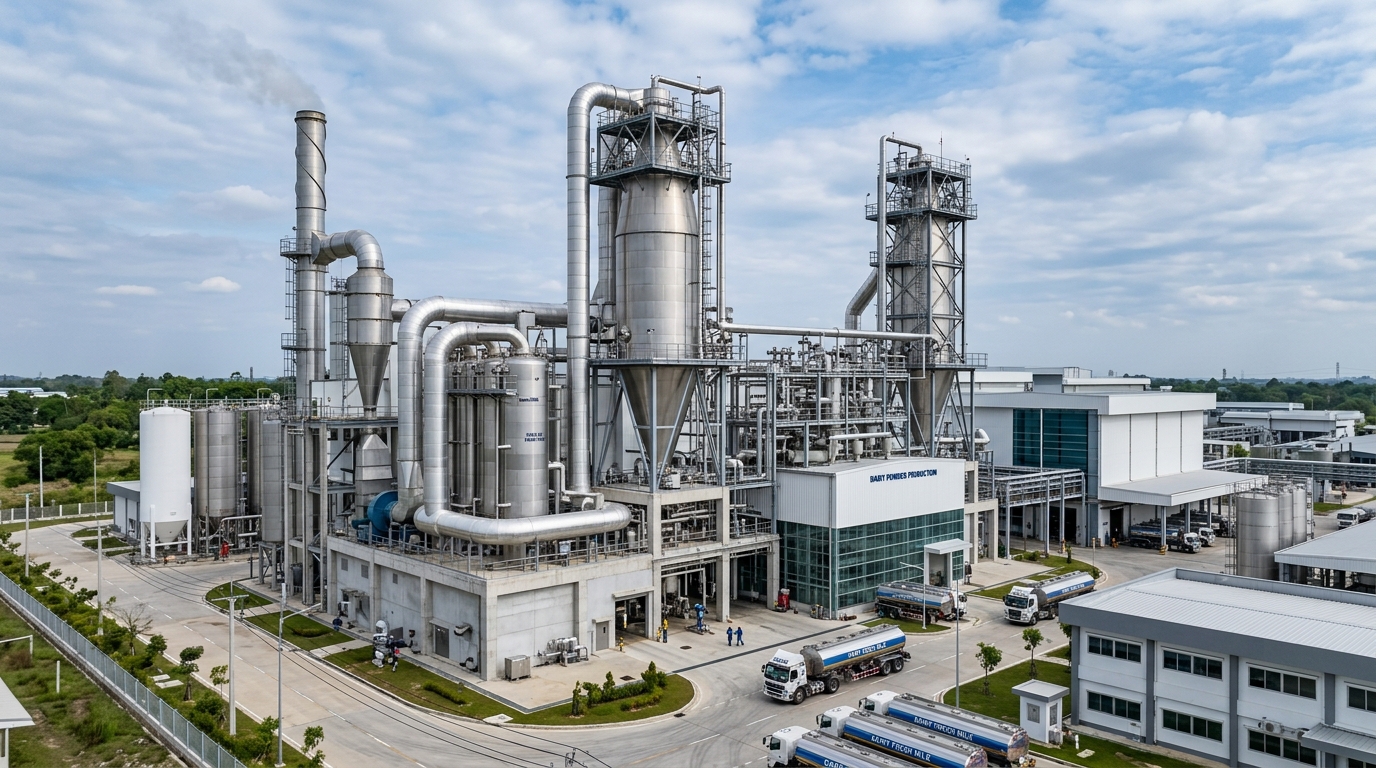
Flue gas and spray dryer exhaust condensing heat recovery system recovering 2.4 MW of low-grade thermal energy to generate continuous 80 °C Clean-In-Place (CIP) washdown and boiler feed preheating for a major dairy processing plant.
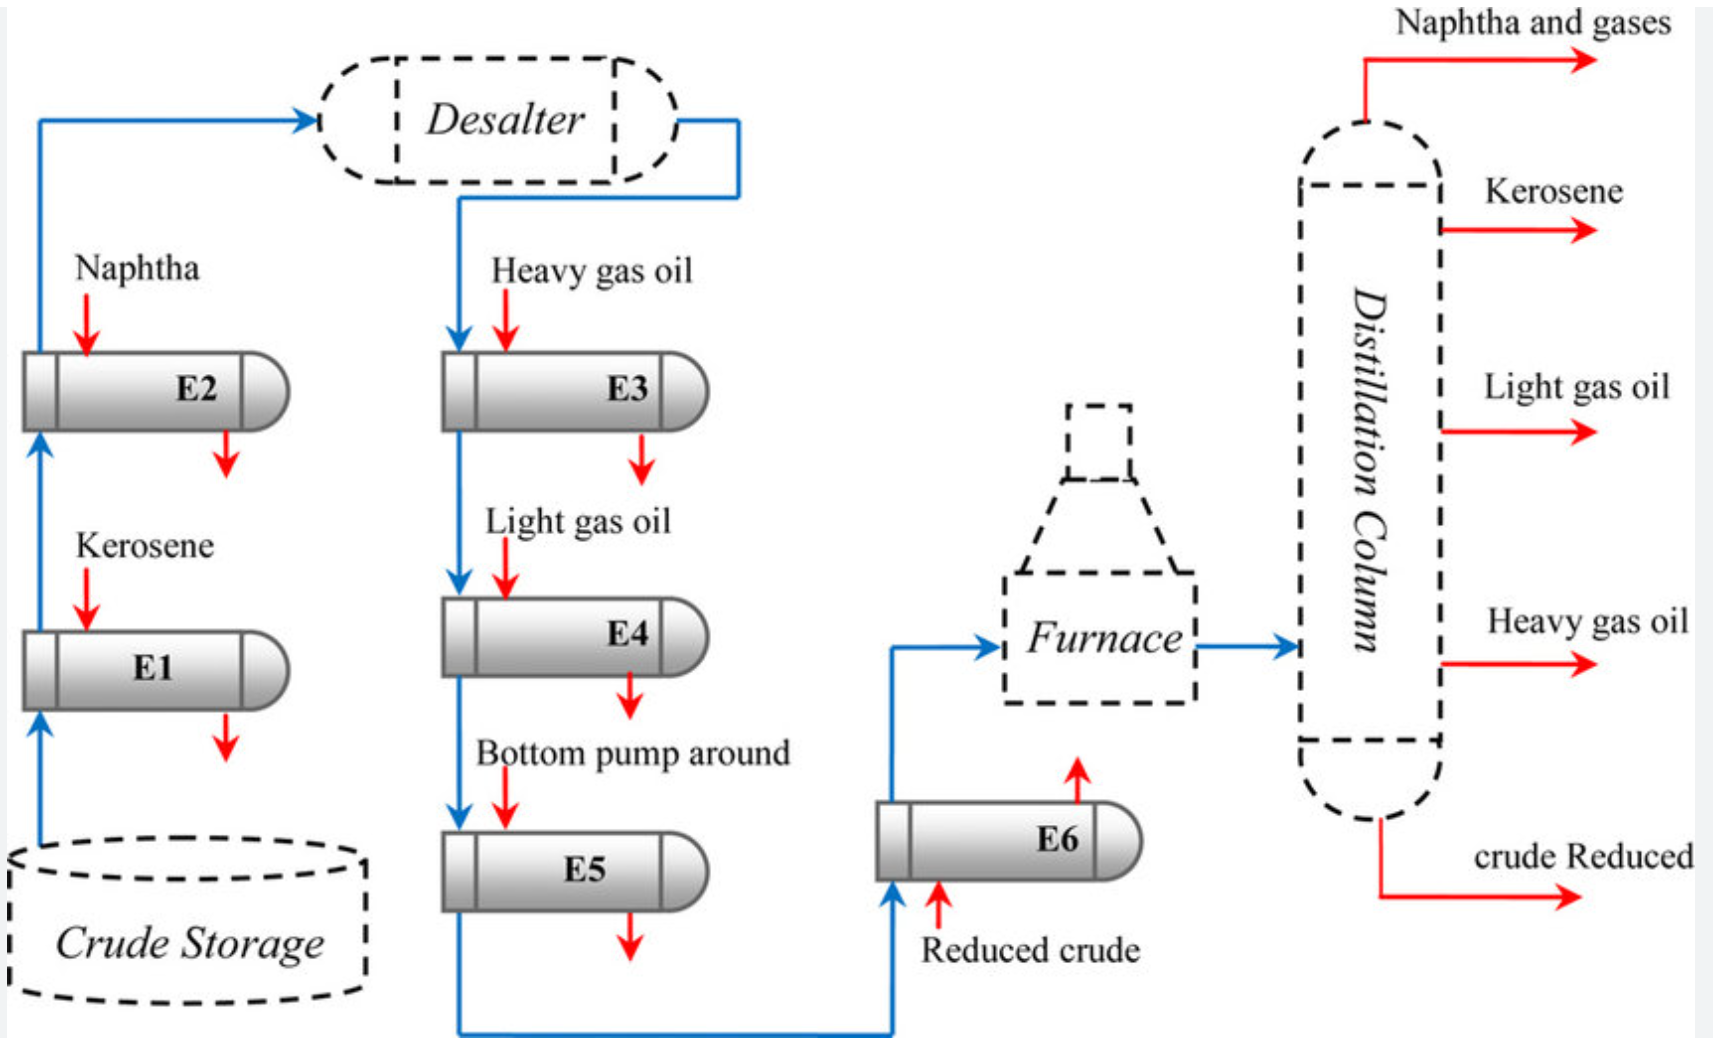
Quantifying energy penalties, furnace duty increases, and carbon emission surges resulting from severe exchanger fouling in a 100,000 kg/h crude distillation unit (CDU).
Industrial boiler flue gas condensing heat recovery system installed on three 15 t/h steam boilers at a commercial brewing facility, capturing waste heat and saving 8 million liters of water annually while cutting natural gas consumption by 16%.
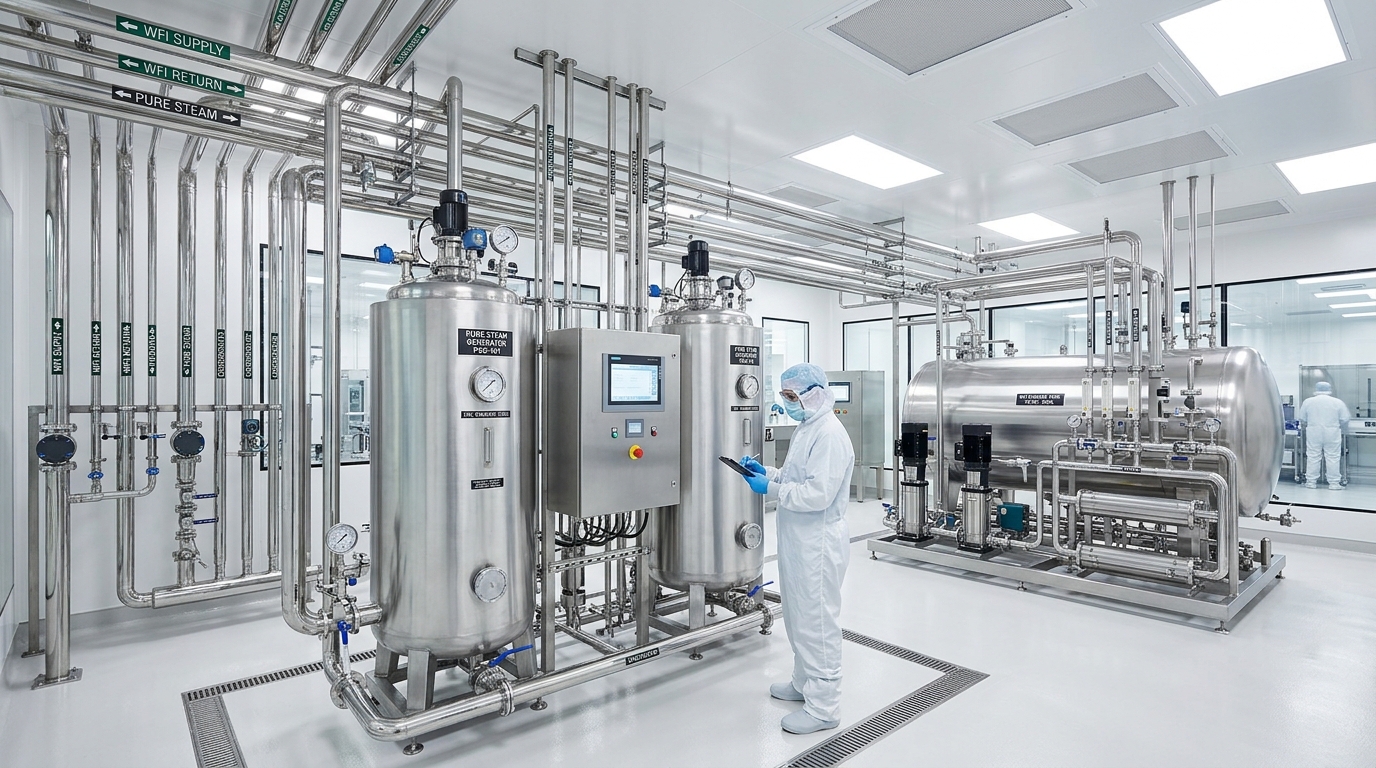
Validation-compliant thermal optimization and industrial heat pump integration recovering low-grade cleanroom HVAC exhaust heat to preheat pure water generation and LTHW loops.
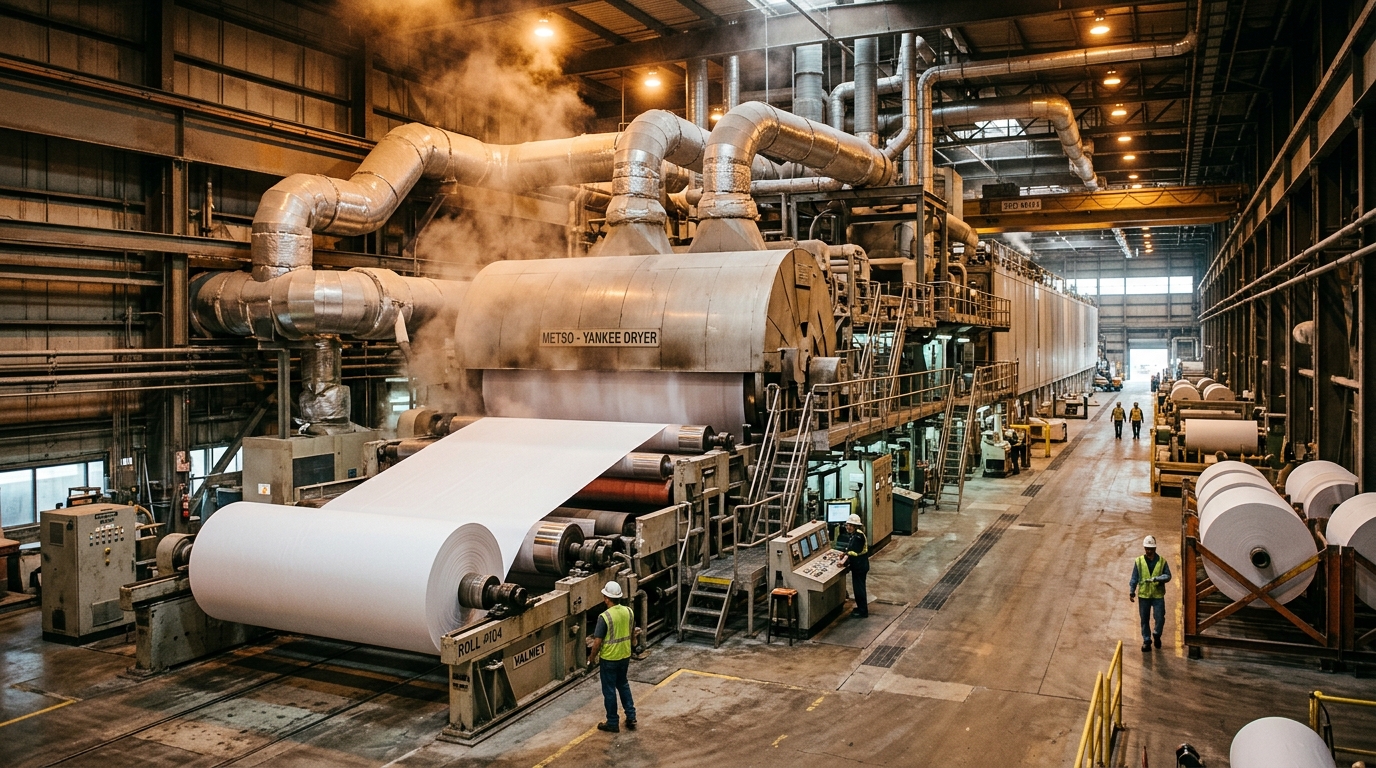
Heavy-duty particulate-tolerant condensing heat recovery system capturing 5.2 MW of waste heat from paper machine Yankee dryer hoods to preheat process water and hall ventilation air.
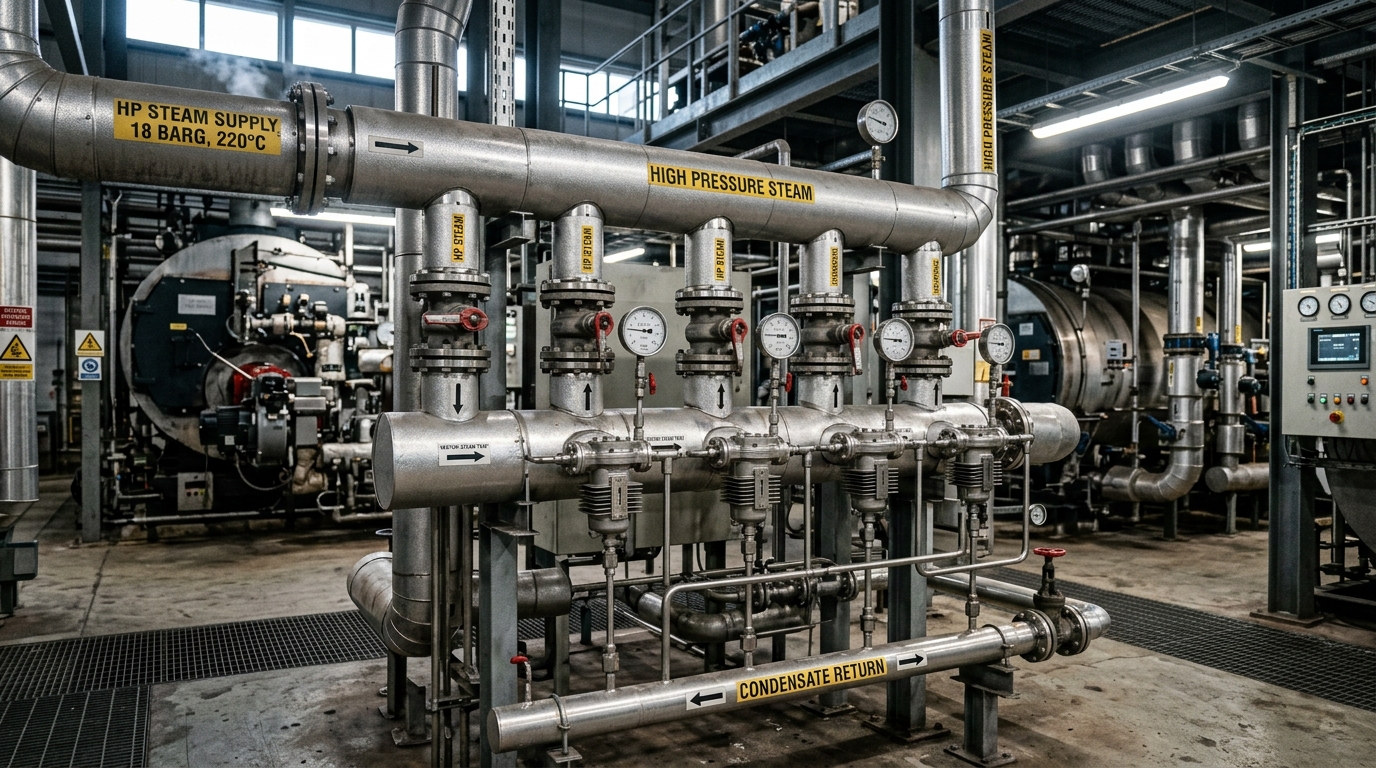
Sitewide steam distribution audit and venturi/orifice permanent steam trap replacement across 340 steam traps, eliminating live steam losses, water hammer, and cutting hospital fuel bills by 12%.
Modeling an industrial post-combustion carbon capture process using 30 wt% aqueous monoethanolamine (MEA) solvent with 98.25% post-flash recovery.
Pinch analysis and heat exchanger network (HEN) retrofit for a crude distillation unit to maximize cross-stream heat recovery.
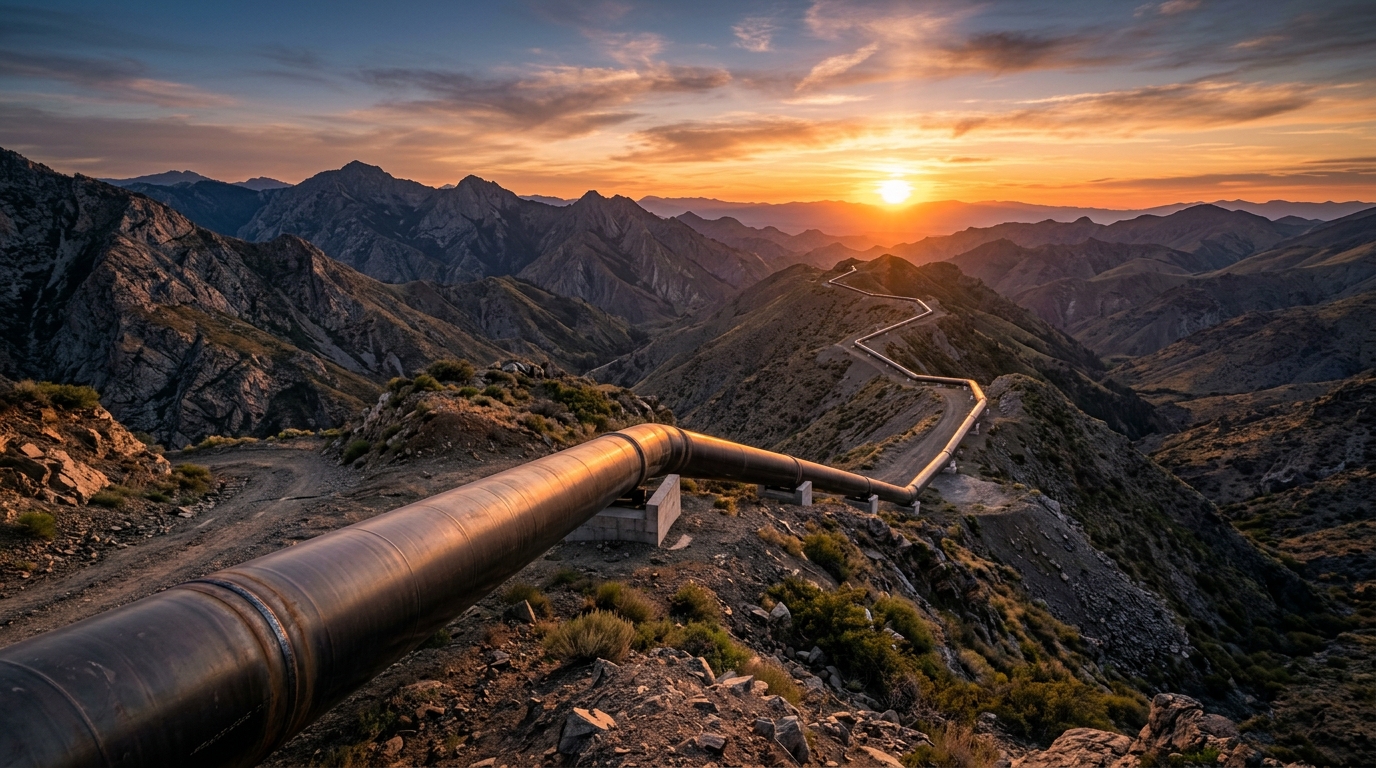
Modeling a 120 km high-pressure natural gas transmission pipeline in Aspen HYSYS, assessing hydraulic pressure drop, elevation/terrain impacts, sizing requirements, and compressor station power.
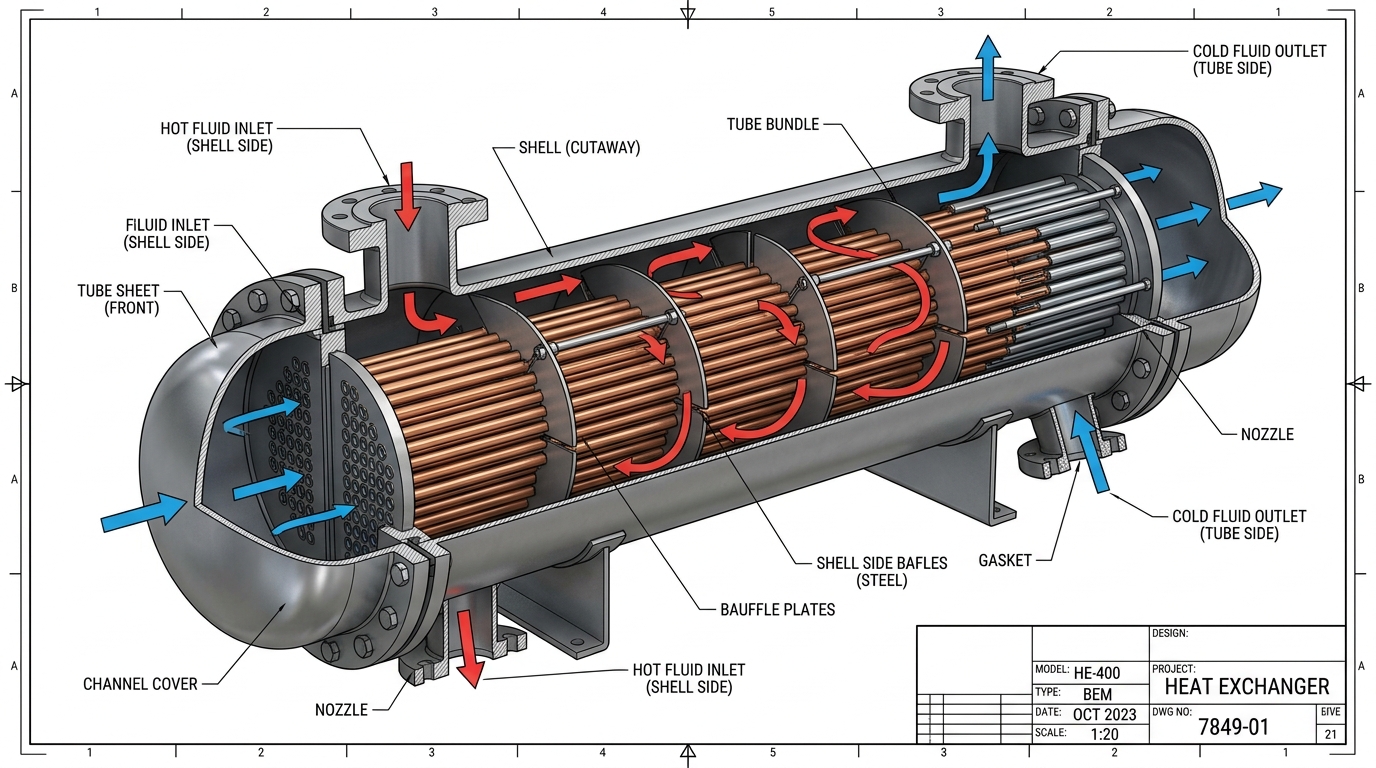
Rigorous thermal & mechanical design rating of TEMA E-type shell-and-tube heat exchangers in Aspen EDR, optimizing baffle cut, tube layout, acoustic vibration, and pressure drop.
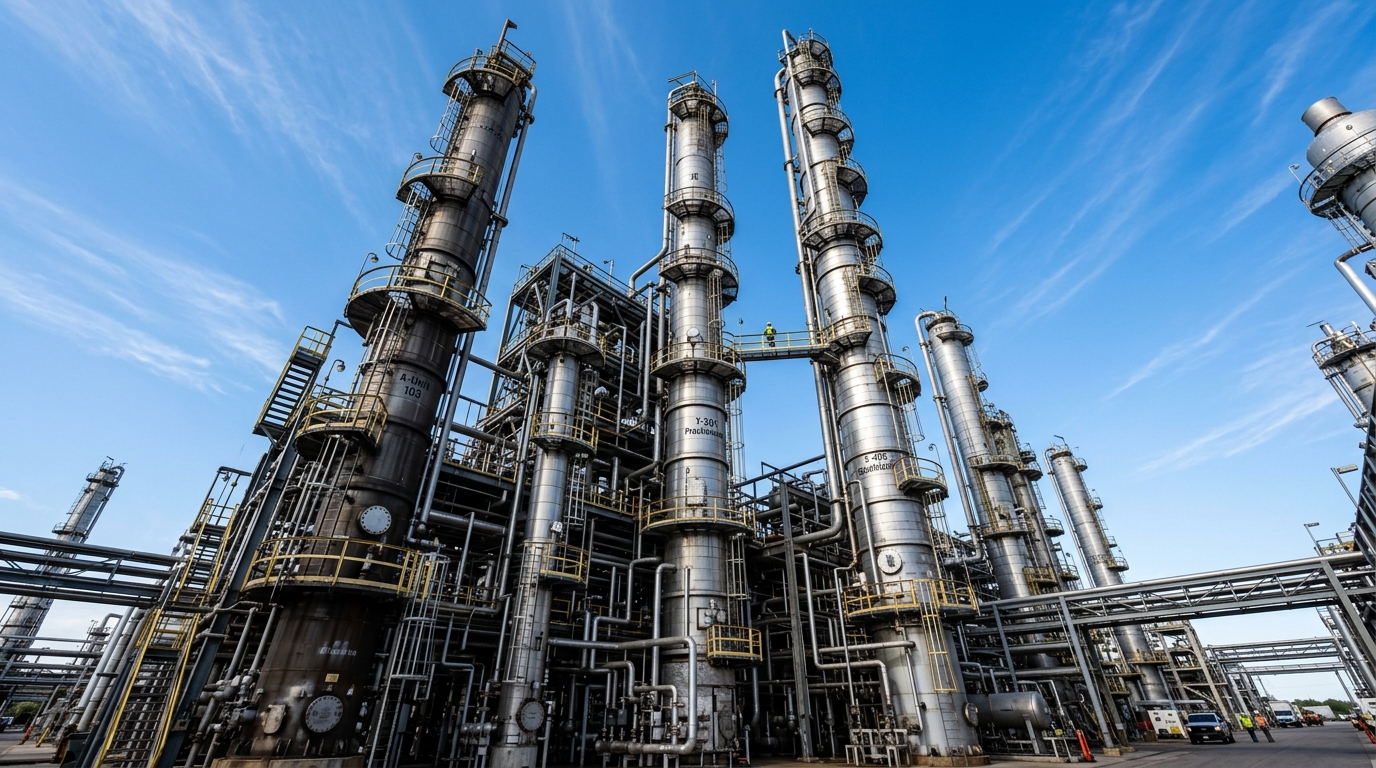
Simulating benzene alkylation with propylene in Aspen Plus, featuring a multi-column distillation train, 99.98% product purity optimization, and unreacted benzene recycling.
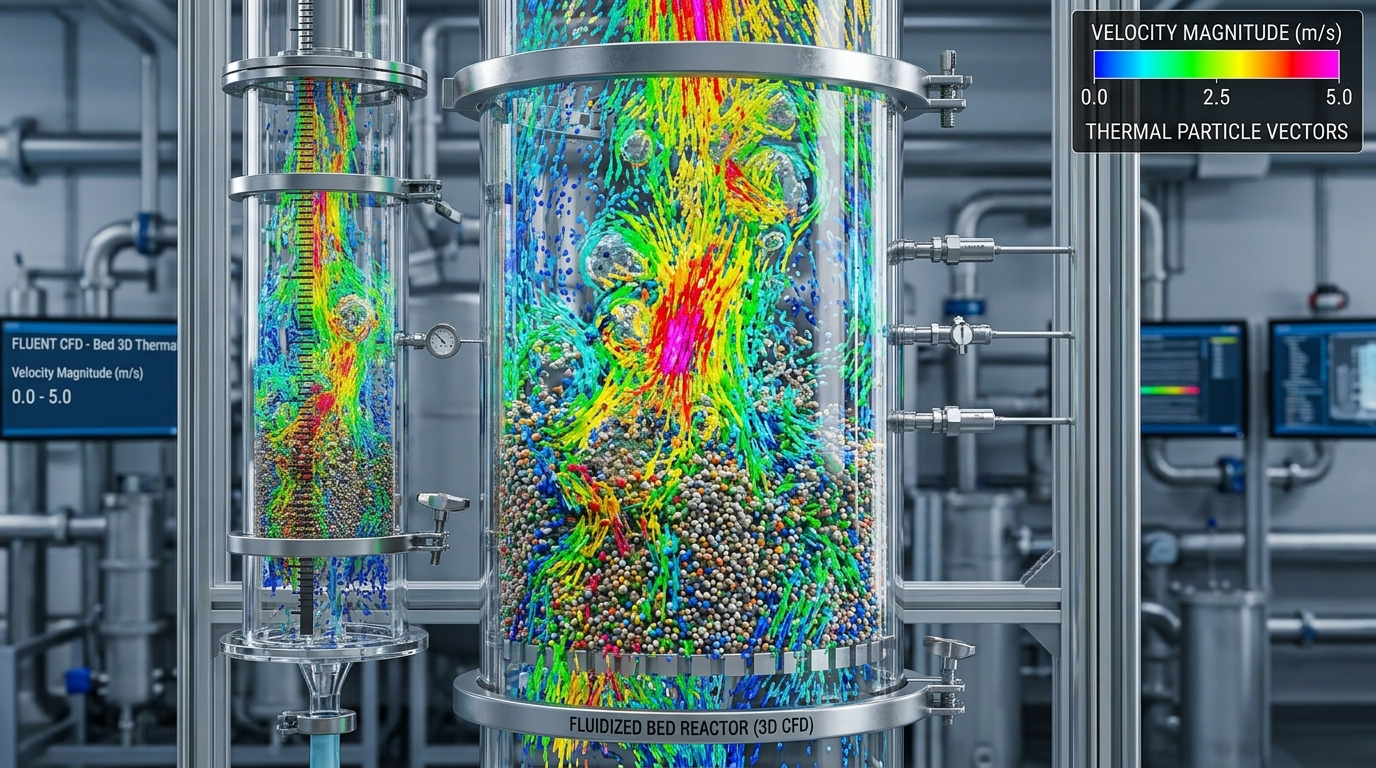
Hydrodynamic simulation of gas-solid fluidized bed reactors in Aspen Plus, evaluating minimum fluidization velocity, bubble dynamics, bed expansion, and cyclone separation.
Thermodynamic simulation of an industrial combined heat and power (CHP) steam plant in Aspen HYSYS, optimizing turbine extraction pressures, boiler efficiency, and condenser cooling.
Thermal & adsorption energy integration study for coastal seawater desalination in Kwale, Kenya, combining Multi-Effect Distillation with Adsorption Desalination (MED-AD).
Solvent extraction and heat recovery process modeling for edible sunflower oil processing in Kisii, Kenya, achieving 99.5% hexane solvent recovery.
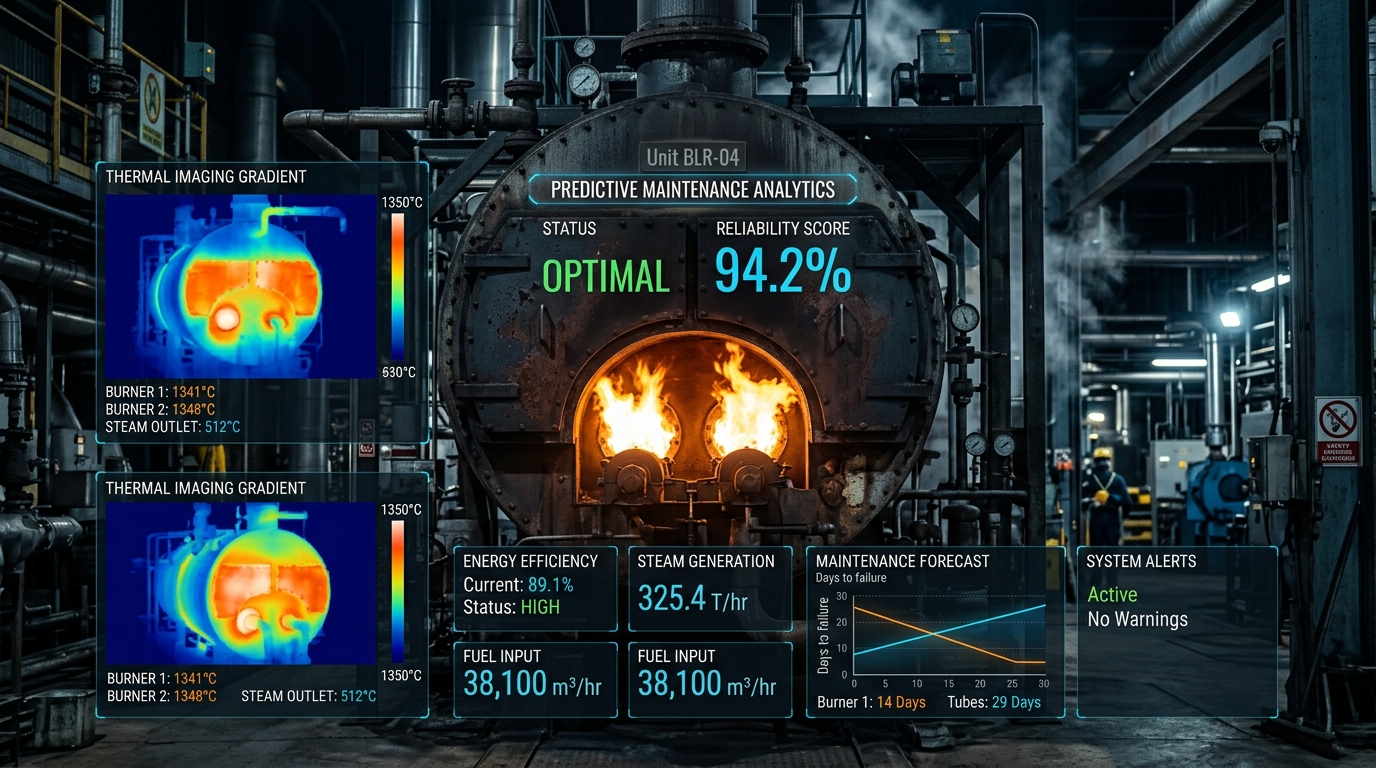
Industrial predictive maintenance and thermal efficiency model developed for Proton Bakers, Zimbabwe, analyzing boiler stack losses, excess O2, and tube scaling.
Need a Custom Simulation Model for Your Site?
We design custom Aspen HYSYS and Aspen Plus digital twins to model your exact process flowsheet, heat exchanger networks, and emissions abatement targets.