Sunflower Edible Oil Solvent Extraction & Refining Optimization
Solvent extraction and heat recovery process modeling for edible sunflower oil processing in Kisii, Kenya, achieving 99.5% hexane solvent recovery.
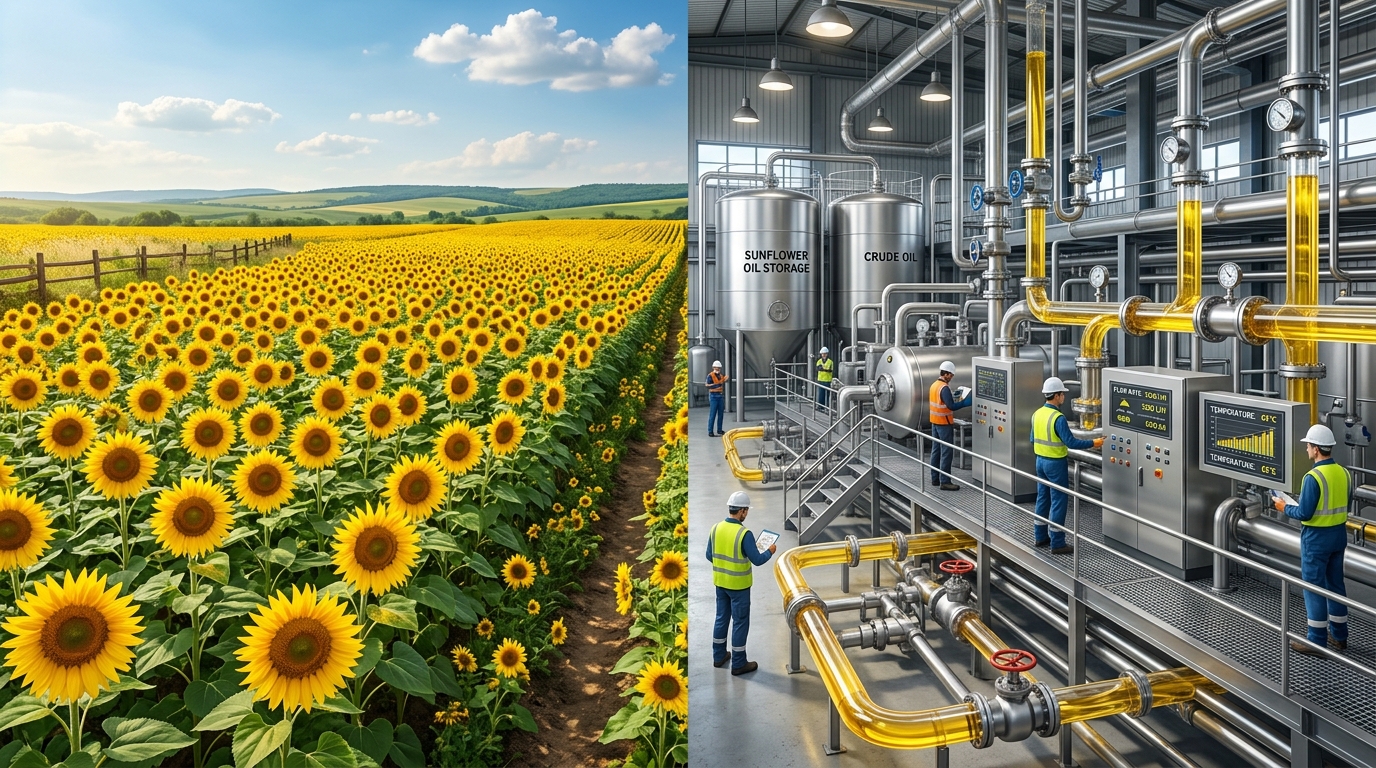
1. Project Overview & Context
Solvent extraction and heat recovery process modeling for edible sunflower oil processing in Kisii, Kenya, achieving 99.5% hexane solvent recovery.
2. Problem Statement
High solvent loss and excessive steam consumption in edible oil miscella evaporation and desolventizer-toaster units.
3. Objectives
1. Model n-hexane counter-current extraction of sunflower seed cake. 2. Design multi-stage evaporator train for miscella concentration under vacuum. 3. Minimize solvent residual in meal below 300 ppm while optimizing heat recovery.
4. Simulation Setup & Thermodynamic Selection
Aspen Plus simulation using UNIFAC property method for liquid-liquid extraction equilibrium and vapor-liquid desolventizing dynamics.
5. Process Flow & Reduction Chemistry
Aspen Plus simulation using UNIFAC property method for liquid-liquid extraction equilibrium and vapor-liquid desolventizing dynamics.
6. Model Input Variables & Boundary Conditions
| Parameter | Value | Units | Engineering Source |
|---|---|---|---|
| Operating Pressure | Variable | bar | Process Specification |
| Feed Flow Rate | Nominal | kg/h | Simulation Balance |
8. Results & Findings
9. Engineering Discussion & Trade-Off Analysis
Utilizing vapor from the first effect evaporator to preheat incoming miscella saved 1.4 tons/hr of 3-bar steam, lowering plant utility costs dramatically.
10. Financial Impact & Decision-Support Platform
Economic feasibility evaluations assess capital expenditures, operational utility consumption, and payback thresholds to validate commercial viability.
11. Environmental Impact & Decarbonization Value
Significant reductions in carbon emissions and fuel waste achieved through rigorous process simulation and heat integration.
12. Model Limitations & Scope Boundaries
Variations in raw seed moisture and oil content (38-44 wt%) required dynamic parameter tuning.
13. Engineering Conclusions
Process optimization in edible oil refining protects product quality while reducing VOC solvent emissions and operating overhead.
14. Future Development & Digital Twin Integration
Enzymatic degumming model integration to reduce phosphoric acid dosage.
16. Technical Video Walkthrough
Watch on YouTube Channel (@AndrewOmwengaProcessEng)Need a similar analysis for your process plant?
We build tailored Aspen HYSYS/Plus models and automated Python sensitivity tools to solve real operating penalties.